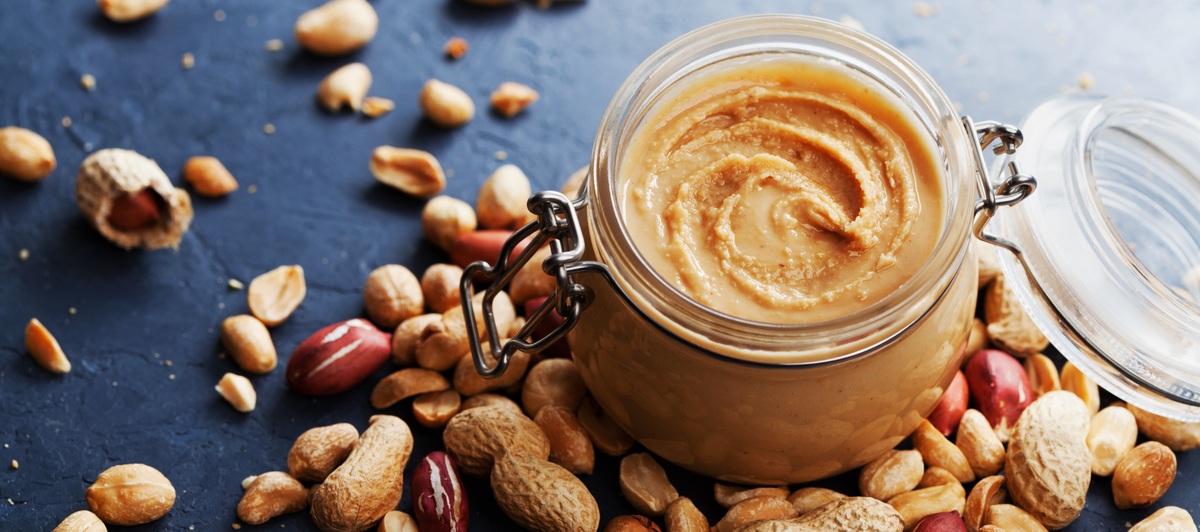
A nut butter grinding machine is not selected based on the capacity alone, since almonds, peanuts, cashews, hazelnuts, pistachios, and seed-based formulations each behave differently under shear, pressure, and heat. A machine that produces a smooth peanut butter at an acceptable throughput may not deliver the same fineness, viscosity, or temperature control with a high-fiber almond butter or a low-oil formulation containing cocoa, sugar, or protein powders.
For commercial producers, the practical goal is repeatable particle reduction without creating excess heat, oil separation, difficult cleaning, or a bottleneck downstream. The right grinding system must fit the product specification and the full production sequence, from raw ingredient preparation through blending, deaeration, filling, and packaging.
What Should a Nut Butter Grinding Machine Do
Nut butter production begins with reducing roasted or prepared nuts into a flowable paste. During grinding, oil is released from the cellular structure of the nut, while solids are reduced to a particle size that determines mouthfeel. The finished butter must also remain sufficiently uniform for pumping, mixing, and filling.
A colloid mill is commonly used as a nut butter grinding machine because it applies high shear in an adjustable rotor-stator gap. Product passes through the grinding zone, where mechanical action reduces particles and disperses solids through the released oil. Depending on the formulation and target texture, the product may make one pass or be recirculated for further refinement.
This operation is more demanding than simply crushing nuts. The mill must process a paste that can become highly viscous, warm quickly, and change flow characteristics as particle size decreases. If the gap is too wide, the butter can feel gritty. If it is too tight or the product is passed through too many times, friction can raise temperature unnecessarily and alter flavor, color, or oil stability.
Start With the Finished Product Specification
The most useful equipment specification starts with what the customer will see in the jar, not with a generic kilograms-per-hour figure. Define the desired texture first: smooth, standard creamy, slightly textured, or intentionally crunchy. A crunchy product often requires separate handling of granulated nut pieces, which are blended into the refined base after grinding rather than sent through the final milling stage.
Oil content has a direct effect on processing behavior. Natural nut butters rely on the oil present in the nuts and may require careful control of roast profile, feed consistency, and recirculation time. Stabilized products can include added oils, emulsifying ingredients, salt, sweeteners, or other dry additions. These ingredients change viscosity and can influence when grinding should occur relative to mixing.
Formulations with cocoa, coconut, plant proteins, fibers, or particulate inclusions require additional attention. Fine powders may need controlled pre-blending to prevent agglomerates. High-solids recipes can demand a more powerful drive, a slower and more deliberate feed rate, or a multi-stage process. A producer making both plain almond butter and chocolate hazelnut spread should not assume one operating setting will serve both products.
Particle Size Is Only One of the Quality Measures
A fine particle size supports a smooth mouthfeel, but it does not guarantee a stable finished product. Oil separation, air incorporation, viscosity, and temperature are equally relevant. Excessive air can affect filling accuracy and contribute to oxidation, which leads to a reduced shelf life. In some processes, vacuum mixing or vacuum homogenization after grinding helps remove entrained air and produce a denser, more uniform butter.
Product temperature should be measured during trial runs rather than estimated from motor power or processing time. Heat generated in the mill may be useful when a formulation needs better flow, but uncontrolled heat is not a process benefit. It can intensify roasted notes, affect heat-sensitive inclusions, and make the product too thin for subsequent controlled filling.
Matching Production Capacity to the Production Line
The published mill capacity is a starting point, not a production guarantee. Throughput varies with nut type, roast condition, particle-size target, viscosity, feed method, and the number of passes. A capacity figure achieved on a free-flowing peanut paste may not be realistic for dense cashew butter or a formulation with added powders.
It is important to size the grinding step around the required output of the next operation. If the filler handles 100 kilograms per hour, the grinding and buffer capacity should supply product consistently without forcing the mill to run at its limit. Operating at the edge of a machine's capability often creates temperature variation, inconsistent texture, and unnecessary downtime.
A practical nut butter production line may include a feed hopper or pre-mix tank, a transfer pump, the grinding mill, and a finished-product tank with agitation. The holding tank provides a buffer between grinding and filling while allowing salt, stabilizers, or crunchy inclusions to be incorporated under controlled mixing. For larger production volumes, multiple mills, recirculation loops, or parallel processing paths may be appropriate.
It is crucial to select the correct transfer pumping system. Nut butter can often be too thick for a centrifugal pump, particularly at lower temperatures or with particulate additions. Positive-displacement pumping is often better suited to viscous products, but the pump, piping diameter, valves, and fittings must all be selected for the actual product rheology. A mill cannot maintain steady performance if it is starved of product or forced to discharge against excessive backpressure.
Feed Preparation Determines Grinding Performance
Grinding cannot correct every upstream issue. Nuts should be properly cleaned, roasted, cooled or conditioned as required, and inspected before entering the mill. Foreign-material control and metal detection are essential safeguards, especially because a narrow rotor-stator gap can be damaged by hard contaminants.
Roast level affects both flavor and grindability. Warmer nuts may release oil more readily, while excessively cold material can produce a stiff paste that is harder to feed and refine. The best handling temperature depends on the nut, formulation, and plant environment. Process trials using the actual raw materials are more reliable than selecting equipment based only on a generic product description.
For producers receiving bulk nuts, upstream equipment may include roasting systems, cooling conveyors, storage hoppers, elevators, and metering devices. A compact startup line may use batch handling and manual loading, while an industrial scale operation may require continuous conveying and automated ingredient dosing. The grinding mill selection should account for the feeding method from the beginning, because inconsistent feeding is a common cause of uneven product quality.
Sanitary Design and Cleaning Requirements
Nut butter is low in water activity, but sanitation remains a critical production requirement. Roasted nuts can carry microbiological risks, and allergen control is especially significant in facilities that process multiple nut types or other food categories. Equipment contact surfaces should be food-grade stainless steel, accessible for inspection, and designed to minimize retained product.
Ask practical cleaning questions before specifying a machine. Can the grinding chamber be opened quickly? How are the rotor and stator accessed? Are seals and gaskets easy to inspect and replace? Can the system be cleaned in place, and is the selected cleaning approach compatible with the product and facility procedures?
Dry cleaning may be preferred between closely related products where water introduction is undesirable. Wet cleaning or CIP may be required for certain formulations and changeover protocols, but it brings the additional requirement of complete drying before production restarts. The best method depends on the allergen plan, validation requirements, product range, and available utilities.
Common Selection Errors to Avoid
The most expensive mistake is choosing a mill solely because it has a high rated capacity. More capacity is not automatically better if the machine cannot hold the required particle-size range, if it overheats the product, or if it creates a cleaning burden that limits useful production time.
Another error is treating nut butter as a single application. Peanut butter, almond butter, tahini, sunflower seed butter, and mixed-nut spreads can require different operating conditions. Products with salt, sweeteners, or added oils introduce further variation. Document the full formula, expected batch size, target viscosity, and packaging temperature before requesting a recommendation.
Finally, avoid planning the mill as an isolated purchase. Grinding performance is tied to roasting, feeding, pumping, post-mixing, storage, and filling. A well-matched standalone unit can solve a targeted problem, but a growing producer should also consider how the machine will connect to the next stage of the line.
Validate the Process Before Purchase
A product trial or test is the most direct way to confirm whether a nut butter grinding machine can meet production requirements. Use the actual nuts, ingredients, and target formulation whenever possible. Record feed temperature, mill settings, throughput, discharge temperature, particle texture, viscosity, and the number of passes needed to achieve the desired result.
The trial should also show how the product moves after grinding. Confirm that it can be pumped to a holding tank, mixed without dead zones, and filled at a stable temperature and consistency. FoodTechProcess can evaluate equipment with customer product samples, helping manufacturers assess both the grinding result and the wider process conditions before committing to a production configuration.
The best machine is the one that produces the required texture at a controllable temperature, supports sanitation and changeovers, and keeps pace with daily operations. When those conditions are verified with real formulation, scale-up becomes a controlled engineering process rather than a capacity estimate.